CNC Machining
CNC Milled Aluminium Housings
Enclosures and gearbox housings milled on 5-axis centres, with bores and seal faces finished in a single fixturing.
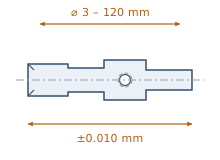
SpecificationsMulti-diameter shafts turned and ground to ±0.010 mm, with the option of hardened and ground bearing seats.
Shafts are turned on 4-axis lathes with bar feeders so unattended running keeps the cost per piece low, then the critical diameters are finish-ground after heat treatment. This two-stage route avoids the concentricity drift you get when a shaft is turned once before hardening and never touched again.
| Process | CNC turning, cylindrical grinding, hardening |
| Diameter range | 3 mm – 120 mm |
| Length range | Up to 600 mm |
| Tolerance | ±0.010 mm on ground diameters |
| Surface finish | Ra 0.4 – Ra 1.6 |
| Concentricity | 0.015 mm TIR typical |
| Materials | 1045, 4140, 20CrMnTi, 304, 316L, 6061 |
| Hardness | Up to 58 HRC on case-hardened seats |
| MOQ | 200 pcs |
| Lead time | 22 – 30 days |
Datasheets and drawings are issued against a part number after technical review, so the revision you receive matches the part we will actually make.
Attach nothing here — send the drawing by reply and we will quote the exact variant you need.
Prefer to skip the form? Email the drawing to our quoting desk.
Enclosures and gearbox housings milled on 5-axis centres, with bores and seal faces finished in a single fixturing.
Specifications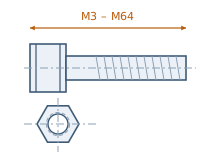
Fully threaded hex bolts in property classes 8.8 to 12.9, cold- or hot-forged and heat treated in house.
SpecificationsCold-formed flange nuts with serrated bearing face for vibration resistance without a separate washer.
SpecificationsSend a STEP file or a PDF drawing with your annual volume. Technical review within one business day, indicative pricing within three.